


This article was automatically translated from the original Turkish version.
Throughout human history, the processing of metals has played a significant role in the development of civilizations. One of the most fundamental techniques to emerge during this process is welding. Welding is nearly as old as the time when humans first began working with metals. Throughout history, it was largely regarded as an art form or a crude construction method. However, scientific advancements in the 19th century and the increasing availability of electrical energy accelerated the development of modern welding.
In 1800, Sir Humphry Davy invented a battery capable of generating an electric current. In 1831, Eugene Desbassyns de Richemont obtained a patent for fusion welding. In 1881, Auguste de Meritens and Nikolai Benardos developed a method to use the heat generated by a carbon electrode electric arc for welding. In 1900, Fouché and Charles Picard produced the first commercial oxyacetylene welding torch. By the 20th century, welding processes began to become increasingly automated.
The types of welding used in aviation are as follows:
MIG welding is a gas shielded welding method that uses inert gases, typically argon or an argon-carbon dioxide mixture, as a shielding gas during the welding process. In this method, a welding wire fed from a spool creates an electric arc with the base material to perform the weld. The inert gases protect the weld pool from atmospheric contamination, resulting in a high-quality, clean weld bead. MIG welding is particularly preferred for materials sensitive to oxidation such as aluminum and stainless steel.
The most important advantages of MIG welding include high welding speed, compatibility with automated welding systems, low smoke production, and ease of application across various materials. However, this method can increase costs due to continuous gas consumption, requires adequate ventilation during welding, and demands precise adjustment of welding parameters to achieve a high-quality result.
MIG kaynak yöntemi-Yapay zeka ile oluşturulmuştur.
TIG welding is a welding method that creates an electric arc between a tungsten electrode and the workpiece. In this method, a thin metal filler rod is used to add material to the weld, while an inert gas such as argon simultaneously shields the weld area. The gas flow prevents the molten metal from coming into contact with air, inhibiting oxidation and enhancing weld quality. Tungsten Inert Gas welding is especially preferred for welding thin and delicate materials, providing low and controlled heat input during the process.
TIG welding stands out for producing high-quality, clean, and smooth weld beads. It can be applied to many types of metals and delivers particularly successful results with materials such as aluminum, magnesium, and titanium. The low smoke and noise levels during welding improve the working environment. However, TIG welding is a slower process compared to other methods and requires a high level of operator skill, which can increase training time and costs.
TIG kaynak yöntemi-Yapay zeka ile oluşturulmuştur.
Electron Beam Welding is a fusion welding method that uses the heat generated when high-velocity electrons strike the workpiece. In this method, electrons are focused in a vacuum environment and directed toward the base metal, creating intense localized heating. The resulting high temperature melts and vaporizes the metal, forming a deep and narrow molten zone. Because electrons move more freely in a vacuum, electron beam welding achieves deeper penetration than other welding methods, allowing thick sections to be welded in a single pass.
Electron beam welding offers significant advantages such as high penetration depth, low heat input, minimal distortion, and reduced post-weld processing requirements. It enables thick sections to be welded in a single pass and provides high strength with low internal stresses. Additionally, it allows the joining of dissimilar or difficult-to-weld materials. However, its main disadvantages include the requirement for a vacuum environment, high equipment costs, and the need for precise control of the welding process.
Laser beam welding is an advanced technology used for joining materials. In this method, a laser beam is focused with high energy onto the interface between two materials, causing them to melt and fuse. The laser beam enables precise delivery of concentrated energy to the desired area through focused light beams. This welding type joins metal parts by focusing the concentrated energy emitted from the laser source using optical components. Laser welding features high welding speed, low heat input, narrow weld seams, and a small heat-affected zone, making it ideal for very thin and precise welding operations.
The advantages of laser welding include high automation potential, successful welding of diverse materials, low thermal impact, and narrow weld seams. Additionally, laser welding is especially suitable for lightweight metals. However, it has some disadvantages: high initial investment costs, brittle weld seams in hardenable materials, difficulties in welding thick sections, and potential health hazards from laser radiation. Moreover, the penetration depth of laser welding is limited and can be hindered by materials with high reflectivity.
Friction welding is a welding method in which electrical energy is converted into mechanical energy to heat the parts through friction. During this process, the parts are heated by mechanical energy and pressure, and joining occurs at the surface without melting, reaching a plastic deformation temperature. The heating phase causes the surfaces to plasticize, while the second phase, forging pressure, consolidates the bond through a forging action. Friction welding, as a solid-state welding method, produces high-quality welds by removing oxides and contaminants from the surfaces. Joining occurs without melting between the materials.
The advantages of this method include low energy consumption, the ability to join dissimilar metals, high joint strength, absence of slag or oxides, and formation of a fine-grained microstructure. However, disadvantages include limited geometric shape options, increased motor power and pressure requirements for large cross-sections, difficulty in welding large components, and high equipment costs. Therefore, friction welding is particularly suitable for parts with specific dimensions and geometries.
Spot welding is a welding method that joins metal parts by passing an electric current between two electrodes. In this method, the electrodes apply a specific pressure to the metal surfaces and conduct current for a set duration. The current heats and melts the metal, causing the surfaces to fuse. The applied pressure ensures the joining of the weld zone, and a cooling period of several seconds is required after the current is stopped to complete the weld. This process can be automated for rapid, high-efficiency operation with minimal manual intervention.
The advantages of spot welding include short processing times, low cost, and high weld quality. Additionally, digital systems can automatically adjust welding parameters, making the process more precise and repeatable. This increases production efficiency and reduces error rates. However, disadvantages include the difficulty of finding optimal parameters and the risk of poor weld quality due to incorrect settings. Moreover, setting the correct parameters can be time-consuming, and initial setup costs may be high.
Seam welding is an adaptation of resistance spot welding and involves creating a series of overlapping spot welds to form a continuous, leak-tight joint. In this process, rotating copper alloy electrodes are used, and the electrodes remain in contact between each spot. The electrode wheels apply a constant force to the workpieces and rotate at a controlled speed. Welding current is typically applied in pulses, although continuous current may be used in some high-speed applications. Seam welding equipment is generally stationary, and the parts to be welded are placed between the electrode wheels. This process can be automated, and various types of seam welding exist, such as wide-wheel seam welding, narrow-wheel seam welding, and seam welding using wire.
The advantages of seam welding include high welding speeds, effectiveness in welding coated steels, and the ability to support high-volume production. For example, it is used in manufacturing tin cans and vehicle fuel tanks. However, this method may be limited by component shape and electrode wheel accessibility. Additionally, there are some limitations regarding material weldability, but most production issues can be resolved with proper adjustments and process control. Risks associated with seam welding include finger and hand crushing hazards, burns from spattered metal, and eye injuries. When welding coated steels or organic materials, fume generation must be controlled and appropriate safety measures must be implemented.
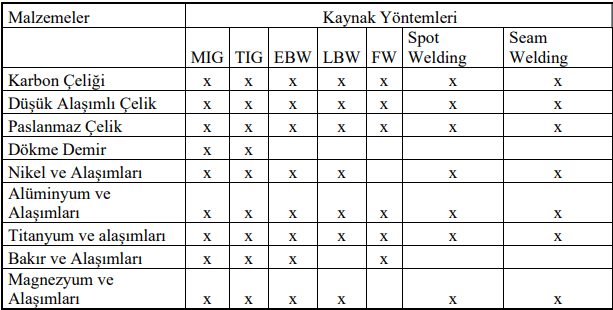
Havacılıkta kullanılan kaynak çeşitlerinin uygulandığı malzemeler tablosu (Hazırlayan ve düzenyelen: Yusuf Cantürk)
Aydın, M. (2003). ELEKTRON IŞIN KAYNAK YONTEMi. Journal of Science and Technology of Dumlupınar University(005), 213-227.
Baştekeli, E. O. "Havacılık Alanında Kullanılan Birleştirme Yöntemleri." *Mühendis ve Makina* 61, no. 699 (2020): 154–169.https://doi.org/10.46399/muhendismakina.767267
Dede, A., Soy, U., & Aslanlar, S. (2002). SÜRTÜNME KAYNAK YÖNTEMİ. Sakarya University Journal of Science, 6(1), 7–12.https://doi.org/10.16984/saufbed.86148
K. Aydın and İ. Karaağaç, "Lazer Kaynağı ve Lazer Kaynağının Başlıca Uygulamaları", ECJSE, c. 5, sy. 2, ss. 693–705, 2018, doi:10.31202/ecjse.379958
Pekşin, S., & Serttaş, S. (2023). Evaluation Of The Resistance Spot Welding Process With KNN and CART Machine Learning Techniques. International Journal of Engineering Technology and Applied Science, 6(2), 132-145.https://doi.org/10.53448/akuumubd.1302120
Thomas Eagar. "Welding Process for Aeronautics". Accessed May 7, 2025.
Westermans, "Resistance Weam Welding". Accessed May 7, 2025.
Yaşar, Y. (2023). MIG/MAG, TIG ve elektrik ark kaynak yöntemleri ile birleştirilen AISI1040, AISI316 ve Al5083 malzemelerin mekanik ve mikroyapı özelliklerinin araştırılması. Amasya Üniversitesi, Fen Bilimleri Enstitüsü, Makine Mühendisliği Anabilim Dalı.

No Discussion Added Yet
Start discussion for "Resource Methods Used in Aviation" article
MIG Welding
TIG Welding
Electron Beam Welding (EBW)
Laser Beam Welding (LBW)
Friction Welding (FW)
Spot Welding
Seam Welding